Contaminant Comparison Chart

For a complete list of contaminants that PUR filters reduce, please view our Performance Data Sheets here.


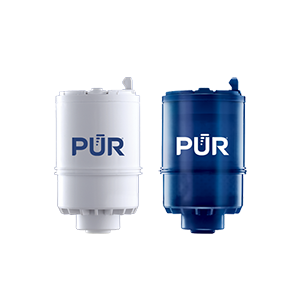
PUR & PUR PLUS FAUCET FILTERS
RF3375/RF9999

View Filters

PUR PLUS PITCHER FILTERS
PPF951K

View Filter

PUR BASIC PITCHER FILTERS
PPF900Z

View Filter


Vs. Brita*

Lead ✓ ✓
Microplastics ✓ ✓
Mercury ✓ ✓ ✓
Chlorine Taste & Odor ✓ ✓ ✓
DEET ✓
TTHM ✓

PUR’s Filtration Systems Are Certified By NSF And WQA For Their Contamination Reduction. WQA certifications as of 5/27/21 for Faucet filter models RF-3375 and RF-9999.

¹ Certified to reduce 10X more chemical and physical substances than Brita’s® leading pitcher filter.
² Certified to reduce 3X more chemical and physical substances than Brita’s® leading pitcher filter.
³ Certified to reduce 2X more chemical and physical substances than Brita’s® leading pitcher filter.
*Versus best-selling Brita® pitcher filter OB03. Brita® is a trademark of Brita LP.
**Like other leading brands, PUR does not filter microbes. As of 3/1/23 Brita® and ZeroWater® were not certified to filter microbes. Brita® is a trademark of Brita LP. ZeroWater® is a trademark of Zero Technologies, LLC..
 

PUR & PUR PLUS FAUCET FILTERS


PUR & PUR PLUS FAUCET FILTERS
RF3375/RF9999

View Filters


Vs. Brita*

Lead ✓
Microplastics ✓
Mercury ✓
Chlorine Taste & Odor ✓
DEET ✓
TTHM ✓

PUR’s Filtration Systems Are Certified By NSF And WQA For Their Contamination Reduction. WQA certifications as of 5/27/21 for Faucet filter models RF-3375 and RF-9999.

¹ Certified to reduce 10X more chemical and physical substances than Brita’s® leading pitcher filter.
² Certified to reduce 3X more chemical and physical substances than Brita’s® leading pitcher filter.
³ Certified to reduce 2X more chemical and physical substances than Brita’s® leading pitcher filter.
*Versus best-selling Brita® pitcher filter OB03. Brita® is a trademark of Brita LP.
**Like other leading brands, PUR does not filter microbes. As of 3/1/23 Brita® and ZeroWater® were not certified to filter microbes. Brita® is a trademark of Brita LP. ZeroWater® is a trademark of Zero Technologies, LLC..


PUR PLUS PITCHER FILTERS


PUR PLUS PITCHER FILTERS
PPF951K

View Filter


Vs. Brita*

Lead ✓
Microplastics ✓
Mercury ✓
Chlorine Taste & Odor ✓
DEET
TTHM

PUR’s Filtration Systems Are Certified By NSF And WQA For Their Contamination Reduction. WQA certifications as of 5/27/21 for Faucet filter models RF-3375 and RF-9999.

¹ Certified to reduce 10X more chemical and physical substances than Brita’s® leading pitcher filter.
² Certified to reduce 3X more chemical and physical substances than Brita’s® leading pitcher filter.
³ Certified to reduce 2X more chemical and physical substances than Brita’s® leading pitcher filter.
*Versus best-selling Brita® pitcher filter OB03. Brita® is a trademark of Brita LP.
**Like other leading brands, PUR does not filter microbes. As of 3/1/23 Brita® and ZeroWater® were not certified to filter microbes. Brita® is a trademark of Brita LP. ZeroWater® is a trademark of Zero Technologies, LLC..


PUR BASIC PITCHER FILTERS


PUR BASIC PITCHER FILTERS
PPF900Z

View Filter


Vs. Brita*

Lead
Microplastics
Mercury ✓
Chlorine Taste & Odor ✓
DEET
TTHM

PUR’s Filtration Systems Are Certified By NSF And WQA For Their Contamination Reduction. WQA certifications as of 5/27/21 for Faucet filter models RF-3375 and RF-9999.

¹ Certified to reduce 10X more chemical and physical substances than Brita’s® leading pitcher filter.
² Certified to reduce 3X more chemical and physical substances than Brita’s® leading pitcher filter.
³ Certified to reduce 2X more chemical and physical substances than Brita’s® leading pitcher filter.
*Versus best-selling Brita® pitcher filter OB03. Brita® is a trademark of Brita LP.
**Like other leading brands, PUR does not filter microbes. As of 3/1/23 Brita® and ZeroWater® were not certified to filter microbes. Brita® is a trademark of Brita LP. ZeroWater® is a trademark of Zero Technologies, LLC..


China Top Mainshaft Sleeve for Cone Crusher Supplier?

A Mainshaft Sleeve Cone Crusher is a small component with a major job: supporting the mainshaft and helping protect the crusher from wear. In a quarry, the sleeve works under repeated pressure, vibration, and abrasive dust. A poor fit can mean premature wear, unplanned maintenance, and lost production. Details matter.

Demand for reliable mineral processing equipment sits within a wider growth trend. The International Energy Agency’s Global Critical Minerals Outlook 2024 reports that the market value of key energy-transition minerals reached about US$325 billion in 2023, roughly double its value five years earlier. The report does not measure cone crusher parts directly, but it helps explain why dependable crushing equipment remains important to mining supply chains. The USGS Mineral Commodity Summaries also provides annual data on mineral production and markets, useful context when assessing equipment needs.

Choosing a China-based mainshaft sleeve supplier requires more than comparing prices. Buyers should check material specifications, dimensional tolerances, machining quality, inspection records, and whether the supplier can match the crusher model. Ask for measurable evidence, such as inspection reports and material test results. A polished catalog is not proof. Even a capable supplier can miss a detail if drawings, measurements, or operating conditions are unclear. That is worth remembering. This guide outlines practical questions for evaluating suppliers, comparing offers, and reducing avoidable fit and service risks.

China Top Mainshaft Sleeve for Cone Crusher Supplier?

Mainshaft Sleeve Basics: Function, Loads, Lubrication, and Failure Modes

A mainshaft sleeve forms a supporting or protective interface around the crusher’s mainshaft; its exact role depends on the machine design. It must tolerate repeated radial loading as crushing forces shift through each rotation. Hard feed, poor alignment, and sudden load changes can concentrate pressure at one edge. Small defects matter. A faint scoring line can become a hot, worn track.

Lubrication must maintain a separating oil film, not merely wet the surface. Confirm oil flow, temperature, and pressure during operation, then inspect samples for wear debris and contamination. ISO 4406:2021 classifies oil cleanliness using particle counts at three sizes: ≥4, ≥6, and ≥14 μm(c). It provides a reporting method, not a universal cleanliness target for every crusher. Set limits using the equipment manual and operating conditions. A clear-looking oil sample can still contain damaging fine particles.

Common failure signs include scoring, discoloration, uneven wear, and rising operating temperature. Check sleeve clearance and shaft alignment during planned inspections; record measurements so gradual wear is visible. Oil starvation may cause rapid metal contact, while abrasive particles can produce slower grooves. Neither diagnosis is certain from appearance alone. Pair inspection findings with oil analysis and operating records. One detail is easy to miss: a sleeve can look serviceable while its clearance has already drifted beyond the specified range.

Material Benchmark: C93200 Bronze Contains 6.3–7.5% Sn and 6–8% Pb

China Top Mainshaft Sleeve for Cone Crusher Supplier?

C93200 bronze is a tin-lead bearing alloy commonly considered for cone crusher mainshaft sleeves. Its specified 6.3–7.5% tin and 6–8% lead are central to its bearing behavior. Tin contributes strength and wear resistance, while lead can improve machinability and help the material accommodate small particles. The balance is primarily copper, with other elements controlled by the applicable specification.

Composition matters. But it is not the whole story. In service, a sleeve faces sustained pressure, vibration, heat, and changing lubrication conditions. A machinist or buyer should check the material certificate, finished dimensions, surface quality, and fit against the shaft. Keep an eye on oil grooves, too; a clean-looking sleeve can still perform poorly if lubricant cannot reach the contact area. I would not treat the alloy grade as a cure-all. Incorrect clearance or poor alignment can shorten service life, even when the bronze chemistry meets its limits. Suppliers should provide traceable test records and clarify which standard defines their C93200 composition. Good details matter.

Dimensional Control: Check ISO 286 Fits, OEM Clearance, and Runout

A mainshaft sleeve for a cone crusher needs a controlled fit, not just a nominal bore size. Even a small clearance error can affect oil-film stability, heat, and wear. ISO 286-1:2010 defines tolerance grades and deviations for limits and fits, but it cannot set the correct clearance for every crusher. Use the equipment maker’s specified clearance as the governing value. Small numbers matter.

Measure the shaft and sleeve at several positions, including near both ends. Record temperature and measurement location; a cold workshop reading may differ from a warmed assembly. Check radial runout with the sleeve seated on the shaft, using a calibrated dial indicator and a repeatable setup. ISO 1101:2017 provides the framework for geometric tolerancing, including runout. Compare the measured result with the drawing limit, not a generic catalog tolerance. If results vary, inspect the setup before rejecting the part. It’s easy to blame the sleeve too soon.

Tips: Keep a measurement log with instrument ID, temperature, shaft diameter, bore diameter, and runout. Confirm the OEM clearance before machining; a fit designation alone does not capture operating conditions.

China Supplier Audit: Review Casting, CNC Machining, NDT, and Traceability

A supplier audit for a cone crusher mainshaft sleeve should begin at the foundry, not with a polished brochure. Ask how the casting grade is verified and how melt records connect to each production lot. Inspect furnace logs, sampling procedures, and mold condition where practical. Look for clear controls on temperature and defect handling. Small details matter. A smooth surface alone cannot prove sound metal.

For CNC machining, compare the drawing revision with the program and in-process inspection sheet. Check bore diameter, sleeve length, concentricity, and surface finish with calibrated tools. Ask to see recent measurement records, not just a sample part prepared for visitors. Tool wear can shift dimensions; the supplier should show how offsets and rework are recorded. I would ask one more question: who approves a deviation, and where is that approval kept?

NDT evidence should match the part, risk, and agreed acceptance criteria. Review the test method, operator qualification, equipment calibration, and reports for ultrasonic or magnetic-particle testing when specified. A pass stamp without location-specific results is weak evidence. Then trace one sleeve from its melt number through casting, machining, inspection, and packing records. Try it during the audit. If files are scattered, retrieval may fail under pressure. That is a real gap, even when the part looks excellent. No supplier has perfect records; unresolved gaps deserve a clear note, not an assumption that they are harmless.

China Supplier Audit: Cone Crusher Mainshaft Sleeve

Illustrative audit-evidence completeness by quality checkpoint. Scores are example values, not measured results from a specific supplier.

Use the audit to verify casting records, machining inspection results, applicable NDT reports, material-to-part traceability, and final dimensional checks. Replace the example scores with documented evidence collected during the supplier audit.

Supplier Comparison: Verify Drawings, Material Reports, Lead Time, and Warranty

When sourcing a mainshaft sleeve for a cone crusher from China, compare suppliers using the same drawing revision. Ask each supplier to confirm the bore, outside diameter, length, oil-groove layout, fit tolerances, and surface finish in writing. A careful drawing review can catch practical gaps, such as an omitted chamfer or unclear datum. Small details matter.

Request material certificates and heat-treatment records linked to the part or production batch. Check the material grade, hardness range, test method, and traceability. A report without matching batch numbers offers limited assurance. Agree on inspection points before production, including dimensional checks and runout measurement. Compare lead times by milestones: material arrival, machining, inspection, and dispatch. Ask how delays are reported. The warranty should define coverage, claim evidence, response time, and exclusions. Vague promises are hard to use when equipment is down.

Tips: Send a marked-up drawing, request sample inspection records, and confirm packaging protects against corrosion and impact. Keep revisions in one email thread. Easy to overlook, but it can prevent mix-ups.