Contaminant Comparison Chart

For a complete list of contaminants that PUR filters reduce, please view our Performance Data Sheets here.


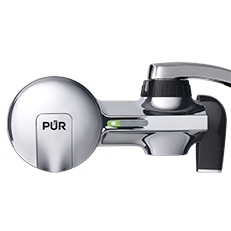
PUR & PUR PLUS FAUCET FILTERS
RF3375/RF9999

View Filters

PUR PLUS PITCHER FILTERS
PPF951K

View Filter

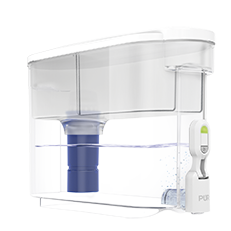
PUR BASIC PITCHER FILTERS
PPF900Z

View Filter


Vs. Brita*

Lead ✓ ✓
Microplastics ✓ ✓
Mercury ✓ ✓ ✓
Chlorine Taste & Odor ✓ ✓ ✓
DEET ✓
TTHM ✓

PUR’s Filtration Systems Are Certified By NSF And WQA For Their Contamination Reduction. WQA certifications as of 5/27/21 for Faucet filter models RF-3375 and RF-9999.

¹ Certified to reduce 10X more chemical and physical substances than Brita’s® leading pitcher filter.
² Certified to reduce 3X more chemical and physical substances than Brita’s® leading pitcher filter.
³ Certified to reduce 2X more chemical and physical substances than Brita’s® leading pitcher filter.
*Versus best-selling Brita® pitcher filter OB03. Brita® is a trademark of Brita LP.
**Like other leading brands, PUR does not filter microbes. As of 3/1/23 Brita® and ZeroWater® were not certified to filter microbes. Brita® is a trademark of Brita LP. ZeroWater® is a trademark of Zero Technologies, LLC..
 

PUR & PUR PLUS FAUCET FILTERS


PUR & PUR PLUS FAUCET FILTERS
RF3375/RF9999

View Filters


Vs. Brita*

Lead ✓
Microplastics ✓
Mercury ✓
Chlorine Taste & Odor ✓
DEET ✓
TTHM ✓

PUR’s Filtration Systems Are Certified By NSF And WQA For Their Contamination Reduction. WQA certifications as of 5/27/21 for Faucet filter models RF-3375 and RF-9999.

¹ Certified to reduce 10X more chemical and physical substances than Brita’s® leading pitcher filter.
² Certified to reduce 3X more chemical and physical substances than Brita’s® leading pitcher filter.
³ Certified to reduce 2X more chemical and physical substances than Brita’s® leading pitcher filter.
*Versus best-selling Brita® pitcher filter OB03. Brita® is a trademark of Brita LP.
**Like other leading brands, PUR does not filter microbes. As of 3/1/23 Brita® and ZeroWater® were not certified to filter microbes. Brita® is a trademark of Brita LP. ZeroWater® is a trademark of Zero Technologies, LLC..


PUR PLUS PITCHER FILTERS


PUR PLUS PITCHER FILTERS
PPF951K

View Filter


Vs. Brita*

Lead ✓
Microplastics ✓
Mercury ✓
Chlorine Taste & Odor ✓
DEET
TTHM

PUR’s Filtration Systems Are Certified By NSF And WQA For Their Contamination Reduction. WQA certifications as of 5/27/21 for Faucet filter models RF-3375 and RF-9999.

¹ Certified to reduce 10X more chemical and physical substances than Brita’s® leading pitcher filter.
² Certified to reduce 3X more chemical and physical substances than Brita’s® leading pitcher filter.
³ Certified to reduce 2X more chemical and physical substances than Brita’s® leading pitcher filter.
*Versus best-selling Brita® pitcher filter OB03. Brita® is a trademark of Brita LP.
**Like other leading brands, PUR does not filter microbes. As of 3/1/23 Brita® and ZeroWater® were not certified to filter microbes. Brita® is a trademark of Brita LP. ZeroWater® is a trademark of Zero Technologies, LLC..


PUR BASIC PITCHER FILTERS


PUR BASIC PITCHER FILTERS
PPF900Z

View Filter


Vs. Brita*

Lead
Microplastics
Mercury ✓
Chlorine Taste & Odor ✓
DEET
TTHM

PUR’s Filtration Systems Are Certified By NSF And WQA For Their Contamination Reduction. WQA certifications as of 5/27/21 for Faucet filter models RF-3375 and RF-9999.

¹ Certified to reduce 10X more chemical and physical substances than Brita’s® leading pitcher filter.
² Certified to reduce 3X more chemical and physical substances than Brita’s® leading pitcher filter.
³ Certified to reduce 2X more chemical and physical substances than Brita’s® leading pitcher filter.
*Versus best-selling Brita® pitcher filter OB03. Brita® is a trademark of Brita LP.
**Like other leading brands, PUR does not filter microbes. As of 3/1/23 Brita® and ZeroWater® were not certified to filter microbes. Brita® is a trademark of Brita LP. ZeroWater® is a trademark of Zero Technologies, LLC..


Why Choose Top Chain Conveyor for Global Sourcing?

Why Choose Top Chain Conveyor for Global Sourcing?

Global sourcing is not simply a search for the lowest equipment price. It is a decision about reliability, maintenance, safety, and long-term operating cost. A Top Chain Conveyor can move cartons, bottles, trays, and packaged goods through demanding production environments. Its modular chain design supports practical layout changes. It can also simplify cleaning and component replacement.

Todd Swinderman, a recognized conveyor-safety specialist, often stresses this principle: “Design for the process, then select the conveyor.” That advice matters when comparing suppliers across borders. Buyers should examine chain material, sprocket quality, frame construction, load capacity, and surface finish. They should request drawings, test records, spare-parts information, and clear installation guidance. A polished catalog is not enough. Real performance appears beside wet floors, uneven loads, frequent starts, and daily washdowns.

Global purchasing still carries uncertainty. Communication can fail. Delivery schedules can shift. A technically strong Top Chain Conveyor may also require local service support and compatible electrical controls. These details are easy to overlook. They should not be.

Experienced buyers often compare total ownership cost, not only the initial quotation. Energy use, cleaning time, wear parts, downtime, and operator access all affect the final result. Some specifications may look impressive but prove unnecessary. Others may be missing. Careful validation remains essential. When suppliers explain limitations honestly, confidence grows. The best sourcing decision may not be the cheapest or fastest one. It is the one that keeps products moving safely and consistently over time.

Why Choose Top Chain Conveyor for Global Sourcing?

Chain Conveyor Fundamentals: Capacity, Speed, Chain Pull, and Duty-Cycle Data

Why Choose Top Chain Conveyor for Global Sourcing?

Chain conveyor selection begins with measurable fundamentals, not catalog appearance. Capacity depends on product weight, chain pitch, loading pattern, and usable width. Calculate mass flow in kilograms per hour, then verify it under real loading conditions. Speed affects impact, noise, and product stability. Heavy loads often move more reliably at moderate speeds. ISO 1977 provides recognized requirements for conveyor chains, attachments, and sprockets. It is a useful baseline, not a complete design.

Chain pull is often misunderstood. Estimate the force needed to overcome friction, elevation, acceleration, and product drag. Add a service factor for starts, stops, and uneven loading. Duty cycle matters too. A conveyor running eight hours daily needs different bearings and motors than one running intermittently. The U.S. Department of Energy reports that motor-driven systems consume about 68% of industrial electricity in the United States. Efficient sizing can therefore reduce operating waste. MHI’s 2024 Annual Industry Report found that 55% of supply-chain leaders planned to increase technology investment. That supports careful automation, but more automation does not fix poor calculations.

Tips: Record actual chain pull with a calibrated sensor during startup and steady running. Check speed at both empty and loaded conditions. Keep a margin, but avoid excessive oversizing. A large motor may hide design errors. Spreadsheet results can still lie. Recheck them against temperature, noise, vibration, and product damage. These imperfect field details often reveal the best sourcing decision.

Engineering Fit: Throughput, Load, Layout, and Energy-Use Benchmarks

Choosing a top chain conveyor starts with engineering fit, not catalogue appearance. The right system should match required throughput, product weight, route length, and operating hours. In practical assessments, I measure peak flow rather than average flow. A line handling 600 units per hour may need capacity for sudden surges, not just 600 units.

Load behavior matters. Heavy pallets create different stresses than small cartons. Check chain tension, transfer points, accumulation zones, and starting torque. Layout also changes performance. Sharp turns, elevation changes, and limited maintenance access can increase friction and downtime. A compact design may save floor space but complicate cleaning or repairs. That trade-off is easy to underestimate. Energy use deserves a real benchmark. Compare motor power, running hours, speed control, and load percentage under normal production conditions. A larger motor is not automatically safer or more efficient. Actual data should guide the choice.

Tips: Record product dimensions and weights for several operating days. Test the heaviest load at startup. Measure noise, speed stability, and energy consumption. Leave access around drive units and inspection points. If the conveyor runs below capacity most of the time, review the specification. My calculations are never perfect; seasonal demand and operator habits can change the result. Build in a realistic margin, but challenge every extra feature.

Global Supplier Screening: ISO 9001, EN 619, CE, and Factory-Test Records

Choosing a top chain conveyor begins with disciplined global supplier screening, not attractive product photos. A capable supplier should provide a current ISO 9001 certificate and explain its quality procedures. Ask who controls incoming materials, welding checks, lubrication, and final inspection. Small details matter.

EN 619 helps assess safety requirements for continuous handling equipment. However, a certificate alone cannot prove every conveyor is suitable for your site. Check the intended load, chain speed, temperature, guarding, and emergency-stop arrangement. CE marking also requires careful review. Request the Declaration of Conformity, technical file references, and applicable risk assessment. Never treat a logo as complete evidence.

Factory-test records add practical confidence. Look for serial numbers, test dates, measured noise, running time, load conditions, and inspector signatures. Photographs of the tested conveyor can connect paperwork with reality. During a factory visit, watch the chain move under load. Listen for irregular impacts. Inspect welds, sprocket alignment, access doors, and protective covers. I have found that neat documents sometimes hide weak process control. That is uncomfortable, but useful. Ask for failed-test records too, if available. Honest suppliers should explain corrective actions without changing the subject. A short video call with production staff may reveal more than a polished sales presentation.

Total Sourcing Cost: Lead Time, Maintenance, Warranty, and Spare-Parts Metrics

Why Choose Top Chain Conveyor for Global Sourcing?

Total sourcing cost extends beyond the purchase price. Lead time, maintenance, warranty support, and spare-parts availability can reshape the final investment. The UNCTAD Review of Maritime Transport 2023 states that maritime shipping carries over 80% of global trade by volume. A delayed component can therefore affect production schedules, inventory buffers, and customer commitments. Top chain conveyor suppliers should provide documented manufacturing lead times, inspection records, and realistic shipping estimates. “Fast delivery” is not enough.

The MHI 2024 Annual Industry Report found that 55% of surveyed supply-chain professionals planned to increase technology investment. This supports evaluating conveyors through lifecycle data, not only initial quotations. Ask for chain wear limits, lubrication intervals, motor efficiency, and preventive-maintenance hours. A useful comparison records annual maintenance labor, planned downtime, and emergency repair frequency. Small details matter. A spare chain stored near the line may prevent several hours of lost production.

Warranty terms also deserve practical review. Confirm coverage periods, exclusions, response times, and whether labor costs are included. The World Bank Logistics Performance Index 2023 assessed logistics performance across 139 economies, highlighting reliability and timeliness as critical supply-chain factors. Spare-parts sourcing should follow the same logic. Require a parts list, stock locations, interchangeability details, and quoted replenishment times. I would not assume the cheapest quotation wins. That assumption often fails when documentation is incomplete, parts are unavailable, or maintenance teams need outside support. One weakness remains: buyers may compare suppliers using estimated data instead of verified operating records.

Why Choose Top Chain Conveyor for Global Sourcing?

5-Year Total Sourcing Cost: Lead Time, Maintenance, Warranty, and Spare Parts

Based on a planning model for a 100-meter conveyor line operating two shifts per day. The top chain conveyor scenario has a higher initial equipment cost, but its shorter lead time, lower annual maintenance requirement, longer warranty coverage, and faster spare-parts availability reduce the estimated five-year total sourcing cost.

Benchmark assumptions: costs are shown in USD; lead-time impact includes estimated production carrying cost; maintenance includes routine service and wear components; warranty reserve covers post-installation risk; spare-parts cost includes commonly replaced chains, sprockets, bearings, and fasteners. Values are indicative planning estimates rather than supplier quotations.

Risk and Compliance Review: ISO 12100, Traceability, and Safety-Test Data

Why Choose Top Chain Conveyor for Global Sourcing?

A top chain conveyor can simplify material movement across warehouses, food lines, and assembly areas. Its value depends on controlled risk, not appearance alone. ISO 12100 provides a practical method for identifying hazards, estimating risk, and selecting protective measures. Review pinch points around sprockets, transfer zones, and return sections. Guards should remain secure during cleaning and routine maintenance. Emergency stops must be accessible, clearly marked, and functionally tested.

Traceability makes supplier claims easier to verify. Request serial numbers, component lists, inspection records, and a documented change history. Safety-test data should show test dates, equipment used, acceptance criteria, and responsible personnel. Generic certificates are weak evidence. A complete file links each result to the exact conveyor configuration delivered.

It should also include load tests, belt or chain tension checks, electrical inspection results, and noise measurements where relevant. One honest limitation matters: test conditions may not match your site. Recheck them before approval.

Tips: Ask for photos of guards, test instruments, and labels. Compare drawings with the shipped unit. Keep records in one controlled folder. Do not accept “passed” without measured values. Small gaps often reveal larger process weaknesses. A supplier may meet the standard on paper, yet overlook operator behavior. Review training, cleaning access, and foreseeable misuse with the same care.