Contaminant Comparison Chart

For a complete list of contaminants that PUR filters reduce, please view our Performance Data Sheets here.


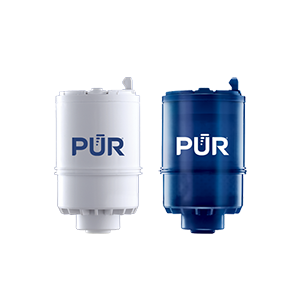
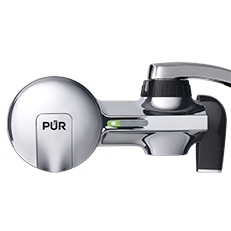
PUR & PUR PLUS FAUCET FILTERS
RF3375/RF9999

View Filters

PUR PLUS PITCHER FILTERS
PPF951K

View Filter

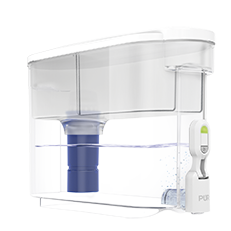
PUR BASIC PITCHER FILTERS
PPF900Z

View Filter


Vs. Brita*

Lead ✓ ✓
Microplastics ✓ ✓
Mercury ✓ ✓ ✓
Chlorine Taste & Odor ✓ ✓ ✓
DEET ✓
TTHM ✓

PUR’s Filtration Systems Are Certified By NSF And WQA For Their Contamination Reduction. WQA certifications as of 5/27/21 for Faucet filter models RF-3375 and RF-9999.

¹ Certified to reduce 10X more chemical and physical substances than Brita’s® leading pitcher filter.
² Certified to reduce 3X more chemical and physical substances than Brita’s® leading pitcher filter.
³ Certified to reduce 2X more chemical and physical substances than Brita’s® leading pitcher filter.
*Versus best-selling Brita® pitcher filter OB03. Brita® is a trademark of Brita LP.
**Like other leading brands, PUR does not filter microbes. As of 3/1/23 Brita® and ZeroWater® were not certified to filter microbes. Brita® is a trademark of Brita LP. ZeroWater® is a trademark of Zero Technologies, LLC..
 

PUR & PUR PLUS FAUCET FILTERS


PUR & PUR PLUS FAUCET FILTERS
RF3375/RF9999

View Filters


Vs. Brita*

Lead ✓
Microplastics ✓
Mercury ✓
Chlorine Taste & Odor ✓
DEET ✓
TTHM ✓

PUR’s Filtration Systems Are Certified By NSF And WQA For Their Contamination Reduction. WQA certifications as of 5/27/21 for Faucet filter models RF-3375 and RF-9999.

¹ Certified to reduce 10X more chemical and physical substances than Brita’s® leading pitcher filter.
² Certified to reduce 3X more chemical and physical substances than Brita’s® leading pitcher filter.
³ Certified to reduce 2X more chemical and physical substances than Brita’s® leading pitcher filter.
*Versus best-selling Brita® pitcher filter OB03. Brita® is a trademark of Brita LP.
**Like other leading brands, PUR does not filter microbes. As of 3/1/23 Brita® and ZeroWater® were not certified to filter microbes. Brita® is a trademark of Brita LP. ZeroWater® is a trademark of Zero Technologies, LLC..


PUR PLUS PITCHER FILTERS


PUR PLUS PITCHER FILTERS
PPF951K

View Filter


Vs. Brita*

Lead ✓
Microplastics ✓
Mercury ✓
Chlorine Taste & Odor ✓
DEET
TTHM

PUR’s Filtration Systems Are Certified By NSF And WQA For Their Contamination Reduction. WQA certifications as of 5/27/21 for Faucet filter models RF-3375 and RF-9999.

¹ Certified to reduce 10X more chemical and physical substances than Brita’s® leading pitcher filter.
² Certified to reduce 3X more chemical and physical substances than Brita’s® leading pitcher filter.
³ Certified to reduce 2X more chemical and physical substances than Brita’s® leading pitcher filter.
*Versus best-selling Brita® pitcher filter OB03. Brita® is a trademark of Brita LP.
**Like other leading brands, PUR does not filter microbes. As of 3/1/23 Brita® and ZeroWater® were not certified to filter microbes. Brita® is a trademark of Brita LP. ZeroWater® is a trademark of Zero Technologies, LLC..


PUR BASIC PITCHER FILTERS


PUR BASIC PITCHER FILTERS
PPF900Z

View Filter


Vs. Brita*

Lead
Microplastics
Mercury ✓
Chlorine Taste & Odor ✓
DEET
TTHM

PUR’s Filtration Systems Are Certified By NSF And WQA For Their Contamination Reduction. WQA certifications as of 5/27/21 for Faucet filter models RF-3375 and RF-9999.

¹ Certified to reduce 10X more chemical and physical substances than Brita’s® leading pitcher filter.
² Certified to reduce 3X more chemical and physical substances than Brita’s® leading pitcher filter.
³ Certified to reduce 2X more chemical and physical substances than Brita’s® leading pitcher filter.
*Versus best-selling Brita® pitcher filter OB03. Brita® is a trademark of Brita LP.
**Like other leading brands, PUR does not filter microbes. As of 3/1/23 Brita® and ZeroWater® were not certified to filter microbes. Brita® is a trademark of Brita LP. ZeroWater® is a trademark of Zero Technologies, LLC..


Why Choose a Belt Annealing Furnace?

Selecting the right heat treatment system can influence product quality, energy use, and production consistency. A Belt Annealing Furnace offers continuous processing for metal strips, wires, tubes, and small components. It moves materials through controlled heating, soaking, cooling, and discharge zones. This steady movement can reduce handling marks and support repeatable results across longer production runs.

Control matters most.

In practical industrial settings, operators monitor furnace temperature, belt speed, atmosphere, and material tension. A stable nitrogen or hydrogen-based atmosphere may help protect clean surfaces, depending on the alloy and approved process design. Properly positioned thermocouples provide useful feedback near critical heating zones. The belt also needs suitable strength, alignment, and resistance to thermal distortion. Small changes can affect hardness, ductility, color, and surface condition.

However, a Belt Annealing Furnace is not automatically the best choice for every factory. Product dimensions, alloy behavior, throughput, available floor space, and maintenance skills require careful evaluation. Initial equipment costs may seem high. Yet lower manual handling and more consistent cycle control can improve long-term operating value. Results still depend on correct calibration, preventive maintenance, and operator training. That point is easy to underestimate.

A reliable selection process should compare furnace design, atmosphere control, temperature uniformity, safety systems, and after-sales technical support. Trial testing with actual materials remains valuable. It reveals practical issues that specifications may not show. This article examines why manufacturers choose belt annealing technology and where its limitations deserve closer attention.

Why Choose a Belt Annealing Furnace?

What Is a Belt Annealing Furnace?

A belt annealing furnace is a continuous heat-treatment system for wire, strip, small parts, and other metal products. Components travel on a moving mesh or solid belt through controlled heating, soaking, and cooling zones. The furnace softens metal, relieves internal stress, and improves ductility after drawing, stamping, or forming.

Temperature control matters. A typical line may use several zones, each with independent burners, heaters, fans, and atmosphere controls. Nitrogen or another protective atmosphere can reduce oxidation on sensitive surfaces. Operators monitor belt speed, furnace temperature, gas flow, and product loading. A small change in belt speed can alter the final hardness. Practical experience shows that uneven loading often creates more defects than the furnace design itself.

Energy performance deserves careful attention. The International Energy Agency reports that industry consumes about 37% of global final energy, making process heating a major efficiency target. The World Steel Association recorded approximately 1.89 billion tonnes of crude steel production in 2023, showing the scale of heat-treatment demand across metal manufacturing. These figures do not guarantee savings for every furnace. A claimed 10% reduction may disappear with poor insulation, frequent start-ups, or excessive air leakage. Product trials, temperature mapping, and measured gas consumption provide more reliable evidence than brochures. The system is powerful, but not automatically efficient.

Why Choose a Belt Annealing Furnace?

A belt annealing furnace provides continuous material handling and controlled thermal processing. The chart shows a representative temperature profile for continuous annealing of stainless-steel products. Actual setpoints depend on alloy composition, thickness, belt speed, and production requirements.

Continuous heating, a stable high-temperature soak, and controlled cooling help improve temperature uniformity, process consistency, and production efficiency compared with manually loaded batch processing.

How Does a Belt Annealing Furnace Work?

A belt annealing furnace moves metal continuously through controlled heating and cooling zones. Its basic job is to soften the material and reduce internal stress. The belt carries each piece at a steady speed. Inside, heating zones raise the temperature gradually, preventing sudden thermal shock. Sensors monitor temperature, belt speed, and furnace atmosphere. Operators compare these readings with production records. The process looks simple.

As the strip or component enters, the furnace warms it to a specified annealing temperature. The material remains there long enough for its structure to change evenly. This holding stage is essential for consistent hardness and flexibility. Controlled cooling follows, often inside the furnace before final exposure to air. Atmosphere control helps limit oxidation and surface discoloration. Without it, the finished surface may require extra cleaning or inspection.

In real production, settings must match material thickness, shape, and loading density. A small speed change can alter the heating time. Overloading the belt can create uneven results. Maintenance also matters. Technicians inspect belt tension, heating elements, seals, and sensor accuracy. They verify actual temperatures instead of trusting displayed values alone. The process is precise, but not self-correcting. Some defects appear only after cooling, which makes review important. Repeatable records help connect furnace settings with hardness tests and surface checks. That practical feedback often leads to better adjustments.

Why Choose a Belt Annealing Furnace? - How Does a Belt Annealing Furnace Work?
Typical operating ranges vary according to material grade, component geometry, loading density, and required metallurgical properties.
Process Dimension Typical Data or Range How It Works Why It Matters
Loading and Conveying Continuous belt transport Parts are placed on a heat-resistant metal or mesh belt and carried through the furnace at a controlled speed. Supports continuous production and provides more consistent processing than manually loaded batch furnaces.
Preheating Zone Approximately 150–500°C Material temperature is increased gradually to reduce thermal shock and prepare the workpiece for the heating zone. Helps minimize distortion, cracking, and uneven temperature distribution, especially in thin or complex parts.
Heating Zone Commonly 500–1,100°C Electric resistance heaters or gas-fired systems raise the workpiece to the temperature required for stress relief, softening, recrystallization, or process annealing. The required temperature depends on the alloy and the intended metallurgical result. Steel, copper, aluminum, and stainless steel use different temperature ranges.
Soaking Zone Typically 10–120 minutes The workpiece remains within a controlled temperature zone long enough for heat to penetrate the section and for the desired metallurgical transformation to occur. Improves hardness uniformity, ductility, dimensional stability, and repeatability throughout the production batch.
Protective Atmosphere Air, nitrogen, hydrogen-containing, or other controlled atmospheres Atmosphere control reduces oxidation, scaling, decarburization, or contamination when the material or surface finish requires protection. Allows the furnace to process parts that need a cleaner surface and reduces post-treatment cleaning or machining.
Belt Speed Often adjustable from approximately 50 mm/min to 5,000 mm/min A variable-speed drive controls the time each workpiece spends in the preheating, heating, soaking, and cooling zones. Flexible belt-speed adjustment enables the same furnace to handle different part sizes, materials, production rates, and heat-treatment cycles.
Cooling Zone Controlled cooling from process temperature to handling temperature Parts are cooled gradually or under a controlled atmosphere after annealing. Forced-air or water-cooled sections may be used where appropriate. Controlled cooling reduces residual stress and helps achieve the targeted hardness and microstructure without unnecessary distortion.
Temperature Uniformity Common design target: ±5–10°C within the working zone Thermocouples, independent heating zones, insulation, and airflow management regulate temperature across the furnace chamber. More uniform temperatures improve part-to-part consistency and reduce the risk of soft spots, overheating, or incomplete annealing.
Production Capacity Determined by belt width, belt loading, belt speed, and cycle time Unlike a batch furnace, the belt system allows parts to enter and exit continuously while different zones operate simultaneously. Suitable for medium- to high-volume production and can reduce handling time between heat-treatment cycles.
Energy Efficiency Improved through zoned heating, insulation, and heat recovery Only the required zones are heated, while insulation and controlled airflow limit heat loss. Some systems recover heat from exhaust or cooling sections. Can lower energy consumption per processed part compared with poorly insulated or frequently opened batch equipment.
Process Monitoring Temperature, belt speed, atmosphere, pressure, and alarms Instrumentation records key operating conditions and alerts operators when a parameter moves outside its set range. Provides traceability, supports quality control, and helps identify process deviations before large quantities of parts are affected.
Best-Fit Applications Fasteners, stamped parts, wire products, small castings, tubes, and continuous strip materials Parts are loaded in a stable, single layer or controlled arrangement so that heat and atmosphere can reach the product effectively. The design is especially useful when consistent throughput, repeatable heat exposure, and reduced manual handling are priorities.

What Materials Can It Process?

Why Choose a Belt Annealing Furnace?

What Materials Can It Process?

A belt annealing furnace supports continuous heat treatment for many metal products. It commonly processes stainless steel, carbon steel, copper, brass, and aluminum. These materials may arrive as strips, wires, sheets, stamped parts, or small formed components. The belt moves each load through controlled heating, soaking, and cooling zones. This steady process can improve softness, ductility, and stress relief.

Material thickness matters. Thin copper contacts heat quickly, while heavier steel parts need longer soaking. Furnace atmosphere matters too. Nitrogen or hydrogen-rich conditions can limit oxidation when properly controlled.

Copper alloys often need clean, low-oxygen processing to protect surface quality. Aluminum requires careful temperature control because its annealing range can be narrow. Surface finish matters. Coated, oily, or mixed-metal loads should receive testing before production.

Operators should check hardness, tensile behavior, color, scale, and dimensional change after treatment. A belt furnace handles high volumes well, but it is not suitable for every material or shape. Complex parts may overlap and heat unevenly. The first trial is rarely perfect. A small test load can reveal issues faster than a specification sheet. Belt speed, loading density, and calibration all affect results. Engineers should match the belt, atmosphere, and cycle to the alloy, then confirm performance through documented testing.

Why Choose a Belt Annealing Furnace?

Why choose a belt annealing furnace? The answer begins with process control. A continuous belt carries parts through preheating, soaking, cooling, and unloading zones. This steady movement reduces manual handling and keeps heat exposure more consistent than batch loading.

The U.S. Department of Energy’s Industrial Decarbonization Roadmap reports that process heating uses about 51% of manufacturing energy. That figure makes furnace efficiency more than a utility concern. A belt furnace can target heat where the workload needs it, while programmable zones limit unnecessary overheating. Controlled atmospheres also help protect bright metal surfaces from oxidation. In daily operation, operators can adjust belt speed, temperature, and gas flow from recorded process data. Small changes matter.

Repeatability is the practical advantage. Parts enter at regular intervals, travel through a known thermal profile, and leave ready for inspection or the next operation. A 2023 industry report from the International Energy Agency also identifies industrial heat efficiency and electrification as important routes for reducing manufacturing emissions. The furnace itself cannot solve every energy problem, though. Poor loading patterns, leaking seals, or unstable gas flow can erase expected gains.

Choose carefully.
Test real parts.

Experience still matters. A trial run with thermocouples, surface checks, and hardness testing can reveal whether the selected belt width, residence time, and atmosphere actually fit production needs.

How to Select the Right Belt Annealing Furnace?

Selecting the right belt annealing furnace starts with the material, not the advertised heating capacity. Define the alloy, strip width, thickness, target temperature, and line speed. A thin stainless strip may need gentle tension control, while heavier parts demand stronger belt support. Match the furnace length to the required soaking time. A short heating zone can create uneven hardness.

Temperature uniformity matters. Ask for mapping results across the working chamber, not only one sensor reading. Independent thermocouples can reveal cold edges or overheated center zones. Atmosphere control also deserves close attention. Nitrogen, hydrogen mixtures, or other approved gases must suit the material and process. Check sealing performance, dew point control, and exhaust design. Small leaks can change surface quality.

Belt tracking is easy to underestimate. In practical evaluations, a belt drifting only a few millimeters can damage edges or interrupt production. Choose a system with accessible guides, simple tension adjustment, and clear maintenance points. Review cooling control, energy consumption, alarm records, and operator access. Safety interlocks should be tested, not merely listed. I would not trust a brochure alone. Request sample trials using your actual material. Record hardness, color, flatness, and output stability. The cheapest furnace may look reasonable, but repeated adjustments can become costly. A trial may also expose an uncomfortable truth: your planned speed is too high. That discovery is useful before installation.